Choose static or dynamic mixing by testing the actual A/B material pair at the required flow, shot size and production pauses. A static mixer combines the streams through fixed internal elements. A dynamic mixer adds a driven mixing element. The suitable choice is the one that delivers an acceptable mix and cure within the pressure, timing and maintenance limits of the process.
The comparison starts upstream of the mixer. Confirm that the dispensing system delivers the required A/B ratio, then evaluate whether the mixer blends those amounts adequately. These are separate checks.
Separate ratio control from mixing quality
A mixer receives the material that the metering system supplies. More mixing cannot correct an incorrect resin-to-hardener ratio. Conversely, the correct quantities can still produce an uneven blend if the mixing arrangement does not suit the material and operating conditions.
Keep two lines in the trial record: one for A/B proportioning and another for the resulting mix and cure. Confirm the ratio basis from the material supplier's technical data sheet. Do not enter a ratio expressed by mass into a volumetric setup without the material information needed for the conversion.
For broader material considerations, see Veady's epoxy, polyurethane and silicone potting machine guide. This article focuses on the mixing configuration once the material system is identified.
Compare the variables that change the decision
Record the viscosity of A and B separately at the processing temperature. A mixed-viscosity value on its own can conceal a large difference between the components. Also record ratio, flow, shot size, fillers and the time the mixed material can remain workable under the intended conditions.
Equipment suppliers do not describe one universal operating envelope for dynamic mixing. Their available designs differ. bdtronic's mixing-unit guidance identifies viscosity, ratio and pot life as selection inputs. TWI's reactive-adhesive guidance also discusses different mixing arrangements. Use that as a reason to test a particular head, rather than assigning every high-viscosity material to a dynamic system.
| Selection input | Static mixing check | Dynamic mixing check |
|---|---|---|
| A/B viscosity and ratio | Can the selected fixed elements produce a satisfactory blend? | Does the proposed driven head improve the blend under documented settings? |
| Flow and pressure | Can the system deliver the target output through the selected tube? | Can the head, drive and feed arrangement operate within their limits? |
| Shot size | Is retained material and replacement waste acceptable? | Is response at the required shot size repeatable? |
| Production pauses | What replacement or purge procedure is needed before restart? | What cleaning, replacement or restart sequence applies to this design? |
| Acceptance | Does the output meet the agreed mix and cure checks? | Does the output meet the same checks, including after pauses? |
Color uniformity can be a useful observation when the formulation makes it meaningful. It is not a universal substitute for the material supplier's cure or performance checks. Define the acceptance method before comparing sample appearance.
Size the mixer and confirm its interfaces
For a static mixer, the tube geometry, element arrangement and outlet all belong in the selection. Nordson EFD's static-mixer selection guide discusses element count, diameter, material behavior and flow. A longer tube or a higher element count is therefore a change to evaluate, rather than an automatic improvement.
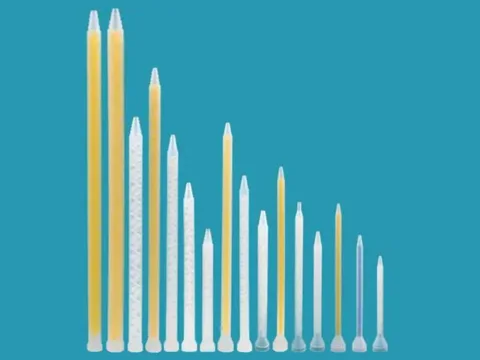
Veady publishes both MS Series static mixers and RS Series dynamic mixers. The following dimensions identify two published examples; they do not establish that either model will suit a particular resin or fit a particular dispensing head.
| Published field | MS06-18 static mixer | RS9-08 dynamic mixer |
|---|---|---|
| Number of sections | 18 | 8 |
| Inner diameter | 6 mm | 9 mm |
| Outer diameter | 10 mm | 12.5 mm |
| Length | 150 mm | 70 mm |
| Outlet inner diameter | 1.5 mm | 3 mm |
| Connection inner diameter | 17 mm | 17 mm |
Check the MS Series static mixer specifications and the RS Series dynamic mixer against the proposed configuration. A matching connection diameter does not prove interchangeability. Confirm the complete interface drawing, seal arrangement, retention method and, for a driven mixer, the drive connection.
Keep flow units consistent. The mixer discussion may use mL/s while the potting process is specified in g/s. Convert only when the relevant material density and measurement conditions are available.
Plan pauses, cleaning and restart
A continuous sample run answers only part of the selection question. Many production cells stop for fixture loading, inspection, breaks or material replenishment. Specify the longest expected pause and test the restart procedure that operators will actually use.
Ask which wetted parts are replaced and which are cleaned, what cleaning materials are approved, and how the first acceptable shot is identified after a pause. Include the time and discarded material in the comparison. Do not assume every dynamic head requires the same cleaning process.
Veady's published references identify DV2030 as a forced-cleaning dynamic valve and DV1216 as a no-clean dynamic valve. Follow the displayed model and version names when requesting documentation. These names describe the listed valve versions; they do not establish that the complete dispensing system has no maintenance tasks.
For each candidate, request the applicable operating and maintenance procedure. Record nozzle or chamber changes, any prescribed purge or cleaning step, the restart check and the consumables required. Select using that complete sequence.
Build a material trial record
Use a record that another engineer can reproduce. Identify the material batches, mixer model, feed arrangement and operating settings. Keep observations separate from pass/fail decisions and retain the evidence supporting each decision.
| Trial field | What to record | Why it belongs in the review |
|---|---|---|
| Material identification | A/B product names, batch and TDS revision | Connects the setup to the tested material. |
| Ratio and viscosity | Mass or volume basis; A/B viscosity in mPa·s with temperature in °C | Prevents unlike material conditions being treated as equivalent. |
| Output and pressure | Shot volume or mass, flow, measurement point and pressure unit | Documents the required operating condition. |
| Mixing configuration | Tube or chamber model; drive settings where applicable | Makes the result traceable to the actual configuration. |
| Pause and restart | Pause duration, procedure, discarded mass and first accepted shot | Tests the interrupted production sequence. |
| Acceptance evidence | Ratio check, mixing observations, cure conditions and agreed test results | Keeps metering, mixing and cured performance distinct. |
Set the sampling plan and acceptance limits with the material and quality teams. If a candidate passes only at a flow the line cannot use, it has not met the production requirement. If it passes continuously but fails after the planned pause, revise and retest the restart procedure before approving the configuration.
The result should identify a working range and the conditions that require an operator action. That gives purchasing something more useful than a claim that one mixing method is always superior.
What to send for a mixer selection review
Provide the A/B TDS and SDS, ratio and its basis, processing temperature, target shot and flow, longest production pause, and the valve or cartridge interface drawing. Add filler information and the agreed mix/cure acceptance method where available. Identify any limits on cleaning materials or disposable components.
Request a mixer configuration review through Veady's existing contact page. Put the operating requirements in the requirements field and email drawings to veady@szweidi.com. Refer to the exact mixer or valve model when one has already been shortlisted.